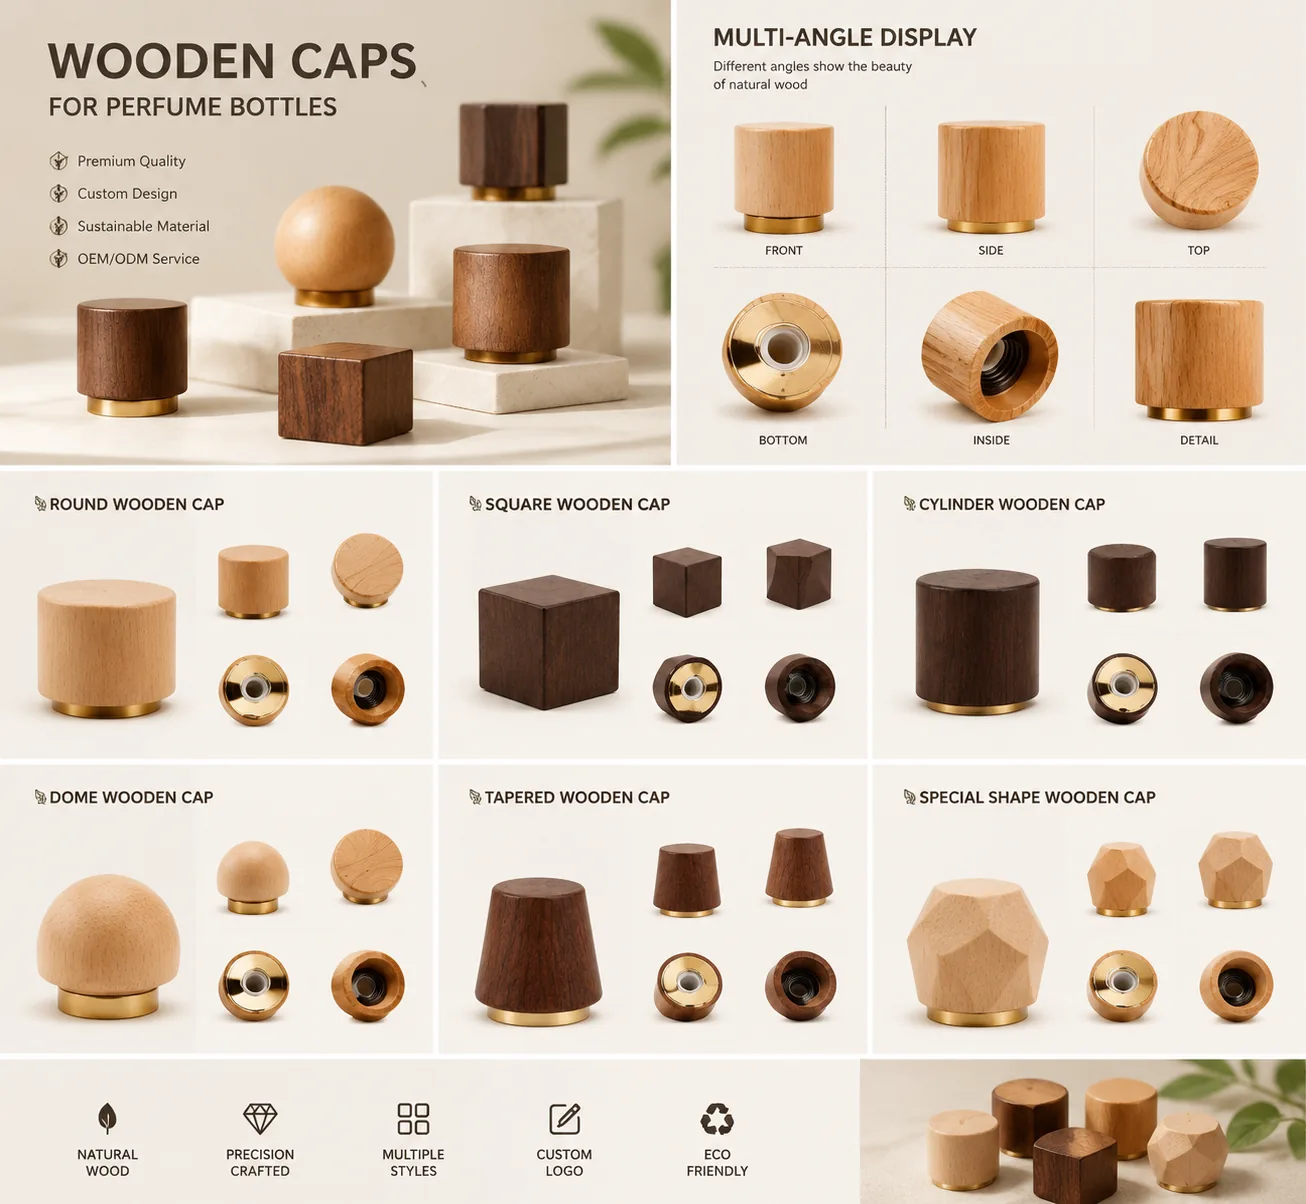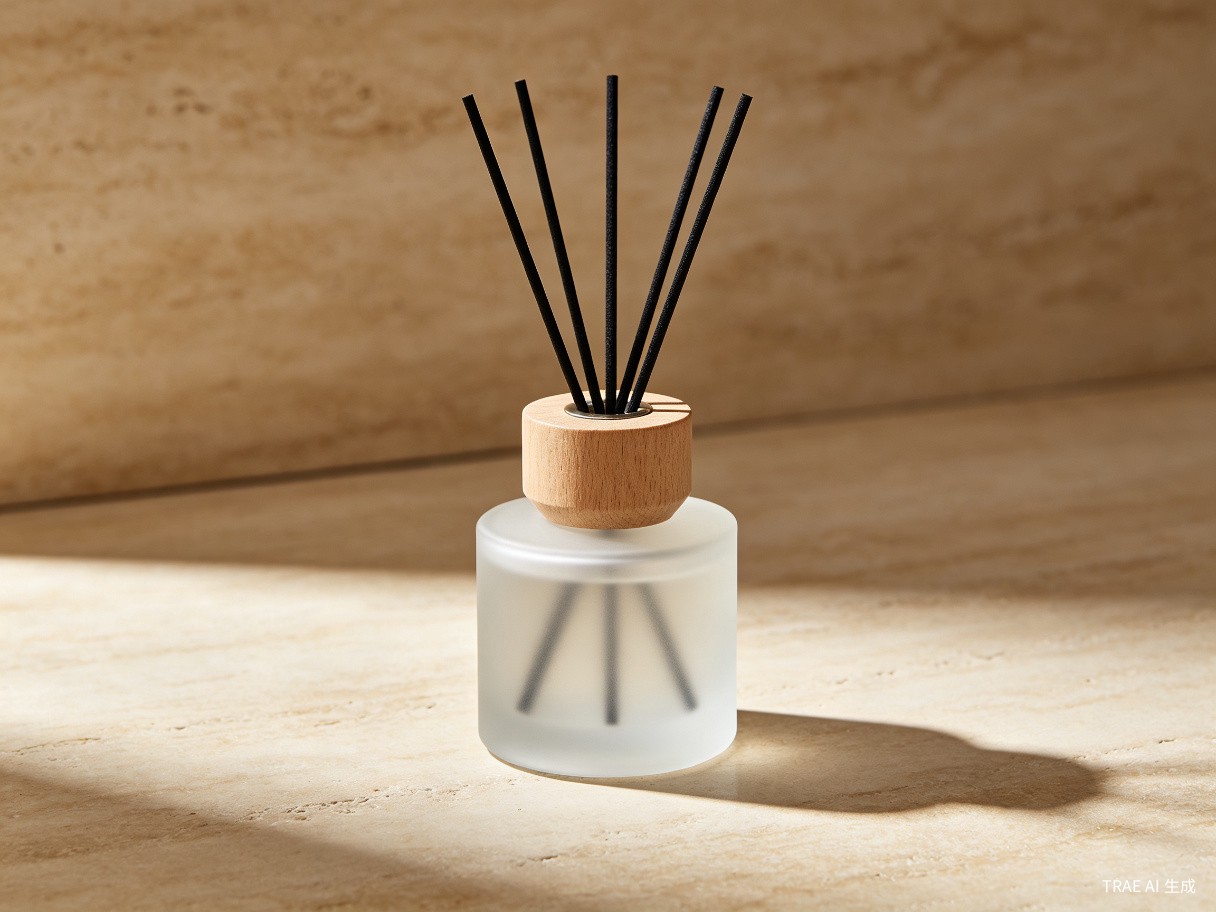
Reed diffusers fail in the same three ways everywhere: the stopper pops out in transit, the closure weeps fragrance onto the carton, or the reeds deliver no scent because the bore is too tight for air to move. All three are decided by dimensions taken before production, and all three are avoidable with a specification sheet that takes an hour to write.
The three interfaces that decide whether a diffuser leaks
- Stopper to bottle neck. The sealing interface. Either a friction fit into the neck bore, or a cap skirt over the neck outside diameter.
- Cap to stopper. If the decorative wooden cap is a separate piece from the functional plug, retention between the two is its own failure mode.
- Bore to reed bundle. Not a seal at all — a controlled opening that sets evaporation rate. Too tight and the product does not perform; too loose and it over-evaporates and sloshes.
Most suppliers quote only the first. The other two are where the complaints come from.
Measure the bottle, not the drawing
Glass neck dimensions carry real tolerance. A moulded bottle specified at 18.0 mm outside diameter may arrive anywhere between 17.7 and 18.3 mm, and ovality of 0.2 mm on a thin-wall neck is normal. A wooden stopper machined to 18.0 mm nominal will be a loose fit on a small bottle and a forced fit on a large one.
The dimensions that matter:
- Neck outside diameter (OD) at the sealing land, measured with a calliper at three heights and two axes
- Bore inside diameter (ID) if the stopper inserts into the neck rather than over it
- Neck height from shoulder to rim — determines how much skirt is available
- Bead or ring position — a retention bead needs a matching groove, not a straight bore
- Wall thickness — thin walls deflect under insertion force, so the effective diameter changes when you push
Best practice: send us three bottles from three production cavities, not one. We machine the prototype to the mean and set the clearance so that the smallest and largest bottle in the sample both pass the pull test.
Common neck sizes and what they imply
| Nominal neck | Typical format | Fit style | Sizing note |
|---|---|---|---|
| 15 mm | Small 50–100 ml diffusers, sample vials | Plug into bore | Tightest tolerance demand; 0.15 mm window typical |
| 18 mm | Standard 100–200 ml reed diffuser | Plug or shallow cap | Most common; specify bore ID from actual glass |
| 20 mm | 200–250 ml, wider reed bundles | Cap over neck | Skirt depth must clear the bead |
| 22 mm | Large-format and car diffusers | Cap over neck | Watch ovality on thin-wall glass |
| 24 mm | Refill bottles, 500 ml + | Threaded or lug | Thread matching is a separate drawing |
Wood moves: the 0.2–0.4% problem
A wooden stopper machined in Guangdong at 30 °C and 80% relative humidity, then air-freighted into a heated European warehouse at 22 °C and 35% RH, will shrink. Across the grain, a 20 mm diameter can lose 0.1–0.3 mm — exactly the clearance you designed in. Now the fit that passed on the bench is loose on the shelf.
Three rules keep this under control:
- Machine from timber at 8–10% moisture content, not air-dried stock at 14%. Kiln-dried and stabilised stock moves far less.
- Design clearance of 0.2–0.4 mm total, split across the diameter, and rely on an elastomer for sealing rather than on wood-to-glass interference.
- Cut across the grain on the sealing face. Radial movement is roughly half of tangential movement, so orient the blank so the tightest dimension runs radially.
Wood-to-glass interference fits are possible and are used on premium closures, but they need a matched moisture spec and a container that does not cycle through a winter. For most programs, an elastomer seal plus a controlled clearance is the more reliable engineering choice.
Seal strategies, ranked by reliability
| Option | Reliability | Cost | Best for |
|---|---|---|---|
| EVA or PE foam disc under the stopper | High | Lowest | Standard diffusers, high volume |
| Cork disc or cork-faced stopper | High | Low | Natural-positioning brands, PPWR-friendly |
| Silicone O-ring in a machined groove | Highest | Moderate | Premium lines, air freight, hot climates |
| Moulded PP plug inside a wooden shell | High | Moderate | When the bore diameter must be exact |
| Friction only, no liner | Low | Lowest | Decorative caps on sealed inner plugs only |
A friction-only wooden stopper is a design decision, not a cost saving, and it should be documented as such. If the inner bottle has its own induction seal or a PP plug, the wooden cap is decoration and the fit can be loose. If it is the only closure, it needs an elastomer.
Evaporation rate is a design parameter, not an accident
The bore diameter sets how fast fragrance leaves the bottle. This is the part buyers most often leave to the factory, then complain about.
- Reed count: 6–10 reeds of 3 mm diameter is the standard range for a 100–200 ml bottle.
- Bore sizing: a bundle of eight 3 mm reeds occupies roughly 56 mm² of cross-section. The bore needs to exceed that bundle with enough annulus for air exchange — typically 12–16 mm bore for an 8-reed bundle, with the opening partly filled by the reeds themselves.
- Too tight: capillary action stalls, the top reeds stay dry, the customer reports “no scent”.
- Too loose: over-evaporation, a bottle that empties in six weeks instead of twelve, and leakage risk when the bottle is laid down.
Test it rather than model it. Fill one bottle with your actual oil, insert the reeds and weigh the whole assembly weekly for four weeks at 23 °C. The slope of the mass-loss curve is your evaporation rate, and it is the only number that matters.
The five-point leak test we run before shipping
- Inverted soak: 24 hours upside down at 23 °C. Any film of oil on the cap face is a fail.
- Heat cycle: 72 hours at 40 °C upright, then 24 hours inverted. This simulates a container in summer and catches thermal expansion failures.
- Vibration: 2 hours on a vibration table at transport amplitude, cap in place. Catches stoppers that walk out.
- Drop: 1.2 m onto a rigid surface, six orientations, in retail carton. Catches cracked skirts and ejected plugs.
- Pull force: measured removal force on a force gauge, recorded per batch. A number in the spec sheet turns “it feels right” into something a QC inspector can check.
Sampling sequence that avoids a re-run
- 3D-printed mock in 2 days — verifies geometry and insertion force before any wood is cut
- Wood prototype in 7–10 days — real species, real finish, real moisture content
- Pilot run of 200–500 pcs — filled and tested with your actual fragrance oil, not water
- Sign-off drawing — with tolerance callouts, moisture spec, liner material and pull-force range
Step three is where most programs discover the problem, and it costs a fraction of discovering it after 20,000 units. Our diffuser stopper range ships with a sign-off drawing as standard; for the sealing trade-offs on jar lids, see the silicone ring versus magnetic closure comparison.
Five line items your spec sheet must contain
- Bottle neck OD/ID with measured range, plus the three-bottle sample reference
- Species, moisture content target, and grain orientation on the sealing face
- Liner material and thickness
- Bore diameter and reed bundle configuration
- Target removal force in newtons, with the test method named
Five lines. It is the difference between a closure that arrives intact and one that arrives as a claim.
Written by
TUOCHEN Editorial
Technical content reviewed by our production engineering team in Guangdong. We have been machining custom wood closures and boxes for fragrance brands since 2012, and we write from drawings and production data rather than from market reports. See the factory.
Need this made to your specification?
We produce custom wooden caps, diffuser stoppers, candle lids and gift boxes from 500 pcs, with FSC certified timber and samples in 7–10 days.